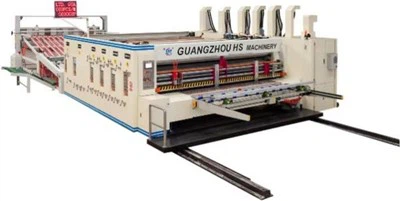


Model:HKM 1636

Tech parameters
| Data/model | 900x2000 | 900x2400 | 1200x24000 | 1200x2800 | 1400x2400 | 1400x2800 | 1600x2800 | 1600x3200 | 1600x3600 |
| Max machine speed(pcs/min) | 300 | 300 | 250 | 220 | 220 | 200 | 200 | 180 | 120 |
| Max feeding size(mm) | 880x2000 | 880x2400 | 1180x2400 | 1180x2800 | 1380x2400 | 1380x2800 | 1570x2800 | 1570x3200 | 1570x3600 |
| Min feeding size(mm) | 280x660 | 280x660 | 320x680 | 320x680 | 360x680 | 360x680 | 420x710 | 420x710 | 420x710 |
| Skip feeding(mm) | 1100x2000 | 1100x2400 | 1500x2400 | 1500x2800 | 1700x2400 | 1700x2800 | 1900x2800 | 1900x3200 | 1900x3600 |
| Max printing area(mm) | 850x2000 | 850x2400 | 1150x2400 | 1150x2800 | 1350x2400 | 1350x2800 | 1540x2800 | 1540x3200 | 1540x3600 |
| Thickness of printing plate(mm) | 7.2 | 7.2 | 7.2 | 7.2 | 7.2 | 7.2 | 7.2 | 7.2 | 7.2 |
Operation Manual for the Paper Feeding Section for Carton box manufacturing machine
The main unit must be started once and the paper feeding portion must go through a reset power-on operation each time the machine is started or following a power interruption caused by an emergency stop/pull-out switch.
1. Close all units and do a zeroing operation to make sure every unit is at zero before setting or modifying the machine's functioning.
⑴ Shut all of the units while the indication light is on and the primary lock is on the right. To zero the main unit, press the zeroing button once; to zero each unit, press and hold the button for three seconds.
⑵ Wait until the machine's primary motor stops at zero before opening it.
2. The paper feeding length can be changed manually using the paper feeding stroke adjustment device on the paper feeding cam box. If the adjustment is greater than the paper's width, an additional sheet might be fed.
3. The size, thickness, and curvature of the paperboard should all be taken into consideration while adjusting the paper feeding suction pressure for Carton box manufacturing machine .
4. To avoid air leakage and inadequate airflow, which could lead to unstable paper feeding, the paper feeding damper needs to be smaller than the length of the paperboard. 5. The size of the back baffle should be changed to correspond with the size of the paper. The back baffle must be raised if the cardboard warps upward, dropped if it warps downward, and reversed if it warps excessively upward.
6. Modify the side baffle to fit the order's specifications. The center blade determines the length of the paper. The drive side setting is the length of the fourth cut plus the fifth cut plus the trimming dimension; the operating side setting is the length of the first slotting cut plus the second cut plus the corner cutting cut.
7. Make the front baffle gap 1.5 times thicker than one cardboard sheet.
8. Set the feed roller gap to either the cardboard thickness minus 0.3 mm or 65% to 70% of the thickness. The steadiness of the paper feeding and the compression resistance needs of the cardboard must be taken into consideration while making adjustments.
9. Place the cardboard evenly and avoid stacking it too high, regardless of its size.
Die-cutting Department Operation Instructions for Carton box manufacturing machine :
1. Adjust the position and clearance of the die-cutting rollers according to the width and thickness of the cardboard.
2. Adjust the die-cutting clearance according to the thickness of the cardboard.
3. Adjust the speed difference according to the wear condition of the die-cutting pads and the precision of the die-cutting plate.
4. Regularly rotate the position of the die-cutting pads, rotating them from the center outwards.
5. For every 150,000 sheets of paper die-cut, the pads require minor re-grinding. The pads must be rotated before re-grinding.
6. If a small area cannot be cut through, or if a small area cannot be cut completely, increasing the die-cutting pressure is not allowed; instead, die-cutting reinforcement is required.
7. Replace dull blades promptly.
8. If blades are loose, reinforce them or replace the die-cutting plate immediately.
Hot Tags: carton box manufacturing machine, China carton box manufacturing machine manufacturers, suppliers, factory, corrugated carton box making machine, Corrugated Box Manufacturing Automatic Plant, Carton Box Manufacturing Plant, Flexo Printing Press Machine, Carton Box Manufacturing Machine, Automatic Corrugated Box Plant